Choosing the right hydraulic gear pump can determine whether a machine runs smoothly or struggles under load. A pump may look suitable on paper, yet fail after weeks of heat, contamination, or pressure spikes. The correct choice depends on more than displacement and price.
Hydraulic systems engineer and author Peter J. Chapple has emphasized, “A hydraulic system must be designed as a complete system, not as isolated components.” This principle applies directly to every hydraulic gear pump selection. Flow demand, operating pressure, fluid viscosity, shaft speed, mounting style, and duty cycle must work together. A pump rated for 250 bar may not survive continuous operation at that level. The detail matters.
This guide presents seven practical tips for choosing a hydraulic gear pump with greater confidence. It considers real workshop conditions, including cold starts, dusty environments, noisy drive lines, and limited maintenance access. It also explains how to read performance curves instead of trusting a single catalog number. Small errors become expensive. Sometimes, the cheapest pump is the costliest decision.
Reliable selection should begin with the manufacturer’s technical data, verified application requirements, and recognized safety guidance such as ISO 4413. Experienced engineers also inspect filtration, oil cleanliness, relief-valve settings, and coupling alignment. These factors are often overlooked. I have seen pumps blamed for failures caused by poor suction piping or contaminated oil. That is an uncomfortable reminder: selection is important, but installation discipline matters just as much.
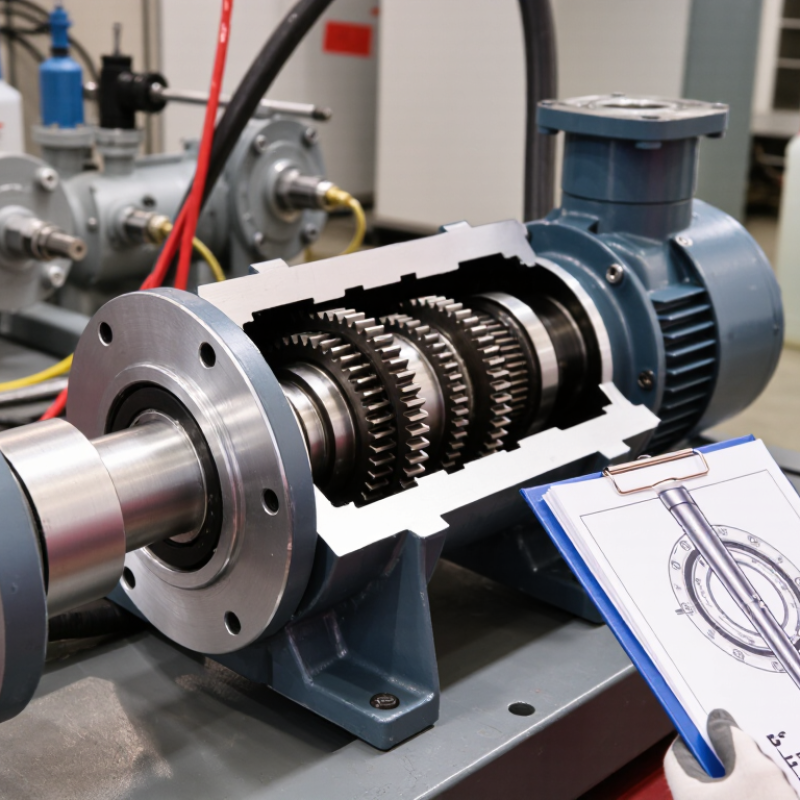
7 Tips to Choose the Right Hydraulic Gear Pump
Understand Your Hydraulic System’s Operating Requirements
Choosing a hydraulic gear pump starts with the machine’s actual operating conditions. Do not begin with pump size alone. Record required flow, working pressure, peak pressure, shaft speed, and operating temperature. Flow affects actuator speed, while pressure determines the torque required at the pump shaft. Measure it carefully. Small errors matter.
Fluid viscosity also deserves close attention. Cold oil can increase resistance during startup, while overheated oil may reduce lubrication and shorten service life. Check the fluid type, contamination level, and filtration quality before selecting the pump. A pump handling clean oil may perform poorly in a dusty environment. I have seen systems fail because operators considered only normal pressure, not cold-start conditions.
Duty cycle is another practical concern. A pump running continuously needs different margins from one used intermittently. Verify continuous and peak ratings separately. Also inspect the drive arrangement, shaft alignment, mounting space, and expected noise limits. A technically suitable pump can still create problems when installation forces enter the shaft. That detail is easy to miss.
Relief-valve settings should match the system’s real pressure limits, not an optimistic estimate. Review the manufacturer’s performance curves, efficiency data, and allowable speed range. If the application changes seasonally, test the pump under both low and high temperatures. A selection worksheet helps, but it cannot replace field measurements. Recheck your assumptions before ordering.
Hydraulic gear pumps must be selected for the system’s continuous and peak pressure demands. The values below show common nominal pressure levels used in hydraulic systems and are intended as an initial selection guide. Always verify the pump’s continuous pressure, peak pressure, speed, displacement, and fluid compatibility before specifying a model.
A pump rated close to the system’s maximum pressure may have limited service life. Select a pressure rating with an appropriate safety margin, while also confirming that the required flow can be delivered at the available drive speed.
Choosing a hydraulic gear pump starts with the machine’s real flow demand, not a catalog number.
Flow determines actuator speed, while displacement determines flow at a given shaft speed.
Use Q = displacement × rpm × volumetric efficiency.
For example, a 25 cm³/rev pump at 1,500 rpm may deliver about 35 L/min after losses. Check the actual speed. Belt slip and engine variation can change the result. Small errors become obvious when a cylinder moves slowly.
Measure the required flow during the hardest working cycle.
A lifting circuit may need 28 L/min, while a steering circuit may need far less. Do not size the pump only for peak flow.
Oversizing can increase heat, noise, and energy loss.
Undersizing causes sluggish motion and longer cycle times.
Leave a practical margin, often around 10 to 15 percent, if the system can tolerate it. That margin is not universal. Machine temperature and duty cycle matter.
Match displacement to the available prime-mover speed, then confirm pressure capability and inlet conditions.
A pump running too slowly may starve the circuit. Excessive speed can shorten service life. Check viscosity during cold starts and normal operation.
I have seen a seemingly correct selection fail because the oil was too cold each morning.
Recheck calculations with measured flow, not assumptions. A flow meter and pressure gauge reveal more than a brochure.
Record speed, pressure, temperature, and cycle time. These details make later adjustments less like guesswork.
Choosing the right hydraulic gear pump starts with its pressure rating, not its advertised maximum. A pump may tolerate peak pressure briefly, yet fail under continuous load. Check the system’s working pressure, pressure spikes, and duty cycle separately. I have seen housings overheat when operators selected a pump by maximum pressure alone. That shortcut looked efficient, but it reduced service life.
Speed range matters just as much. Confirm the pump’s minimum and maximum revolutions per minute, then compare them with the prime mover. Excessive speed can damage bearings, increase noise, and starve the inlet. Low speed may cause weak output, especially with cold or thick fluid. Measure actual shaft speed during startup, normal operation, and heavy demand. Do not rely only on the motor nameplate.
Fluid viscosity and inlet conditions can change the result. A pump rated for a pressure level may still perform poorly with restricted suction piping. Keep the inlet line short, adequately sized, and free from sharp bends. Check the manufacturer’s data for continuous pressure, intermittent pressure, speed limits, and required inlet conditions. A relief valve should protect the circuit, but it is not a substitute for correct pump sizing. One detail is easy to miss: pressure and speed ratings often depend on fluid temperature. Test the system after warm-up, record the readings, and question any result that seems unusually perfect.
| Tip | Selection Dimension | Typical Engineering Reference | How to Select the Pump | Key Verification |
|---|---|---|---|---|
| 1 | Define the Required Flow Rate | Flow is commonly specified in L/min or US gal/min. |
Calculate the required flow from actuator speed, cylinder area, or motor displacement. Select a pump displacement that provides the required flow at the intended operating speed, allowing for volumetric efficiency losses.
Formula: Theoretical flow ≈ displacement × speed. |
Confirm the required flow at minimum, normal, and maximum engine or motor speed. |
| 2 | Choose the Correct Pressure Rating | Common gear-pump operating ranges are approximately 100–250 bar, depending on construction and application. | Select a continuous pressure rating above the system's normal working pressure. The pump's intermittent or peak rating should exceed short-duration pressure spikes, but it should not be treated as a continuous operating value. | Compare continuous, intermittent, and maximum pressure ratings. Set the relief valve within the limits of the lowest-rated component. |
| 3 | Match the Speed Range | Many industrial gear pumps operate roughly between 500 and 3,000 rpm; exact limits vary by displacement, pressure, lubrication, and design. | Ensure the pump's minimum speed is low enough for reliable filling and that its maximum speed is above the highest actual shaft speed. High speed can increase noise, wear, and cavitation risk. | Verify both minimum and maximum allowable rpm, especially when driven by variable-speed engines or electric motors. |
| 4 | Calculate Pump Displacement | Displacement is normally stated in cm³/rev or in³/rev. |
Estimate displacement using:
Displacement ≈ required flow × 1,000 ÷ (speed × volumetric efficiency) For an initial estimate, volumetric efficiency is often treated as approximately 0.85–0.95, then confirmed from the pump performance data. |
Check actual output flow at the intended pressure, temperature, viscosity, and speed rather than relying only on theoretical displacement. |
| 5 | Confirm Fluid Viscosity and Temperature | Mineral hydraulic oils are often selected within approximately 15–46 cSt at operating temperature, while the allowable range depends on the pump design. | Choose a pump compatible with the fluid's minimum start-up viscosity and maximum operating viscosity. Excessively low viscosity can increase internal leakage; excessive viscosity can cause poor filling and high inlet losses. | Verify the approved fluid type, viscosity range, cold-start condition, and maximum oil temperature. A common hydraulic-oil operating temperature range is approximately 30–60°C. |
| 6 | Size the Inlet and Check Cavitation Risk | The pump inlet should be designed for low pressure loss and adequate oil supply; excessive inlet vacuum can cause noise, vibration, and damage. | Use an adequately sized suction line, keep it short, minimize sharp bends, and place the reservoir above or close to the pump inlet when practical. Avoid undersized filters or restrictive inlet fittings. | Confirm inlet pressure or inlet vacuum limits, filter cleanliness, oil level, hose condition, and the required inlet port size. |
| 7 | Verify Installation and Duty Cycle | Pump life depends on pressure, speed, temperature, contamination level, shaft loading, and the proportion of time spent under heavy load. | Select the correct rotation direction, mounting style, shaft configuration, port arrangement, seal material, and drive coupling. For continuous high-load operation, choose a pump with sufficient durability margin rather than sizing only for short-term peak performance. | Confirm filtration, cleanliness level, shaft side-load limits, alignment, relief-valve protection, duty cycle, and maintenance requirements. |
Choosing the right hydraulic gear pump starts with the fluid, not the catalog price. Check the fluid’s viscosity, temperature range, additives, and contamination level. A pump designed for mineral oil may perform poorly with biodegradable or water-based fluids. Ask the fluid supplier for compatibility data. Small seal changes can prevent expensive leakage.
Measure efficiency under real operating conditions. Compare pressure, flow, speed, and expected duty cycle rather than relying on maximum ratings. Volumetric efficiency matters when stable actuator movement is required. Mechanical efficiency affects heat generation and energy use. Keep suction lines short, clean, and adequately sized. Cavitation often sounds like gravel inside the housing. That sound is a warning.
Durability depends on materials, filtration, alignment, and maintenance access. Select corrosion-resistant parts when moisture or aggressive additives are present. Match the pump’s pressure rating to continuous work, not occasional peaks. Install filtration based on the manufacturer’s cleanliness recommendation, then inspect the filter during early operation. I once treated a noisy pump as a normal break-in issue. That shortcut was wrong; restricted inlet flow caused the noise. Check shaft alignment and mounting rigidity as well. A small misalignment can damage bearings over time. Leave room for inspection. Perfect calculations still fail when maintenance is difficult. Evaluate service records, test data, and technical support from qualified suppliers before making the final choice.
Tip 1: Match the pump to the installation space. Measure shaft alignment, port direction, mounting clearance, and suction-line length before ordering. A compact pump is not always the easiest pump to service.
Tip 2: Check actual pressure and flow, not catalog maximums. Continuous operation near the limit increases heat, noise, and wear.
Tip 3: Confirm fluid compatibility, viscosity range, and operating temperature. These details affect efficiency and seal life.
Tip 4: Design maintenance access into the installation. Leave room for filter changes, pressure checks, and shaft inspection. A pump hidden behind guards may save space but increase downtime.
Tip 5: Control contamination carefully. ISO 4406 cleanliness codes provide a practical language for comparing hydraulic-fluid condition. In field service, neglected filtration is a common and expensive weakness. I have seen clean-looking oil damage components quickly.
Tip 6: Compare total cost, not purchase price. The U.S. Department of Energy reports that pumping systems can consume nearly 20% of industrial electricity. Hydraulic efficiency, motor loading, leakage, and heat rejection all influence operating cost.
Tip 7: Estimate the full life-cycle cost. Include installation labor, filters, seals, oil analysis, energy, and planned downtime. A higher-priced pump may be cheaper over five years. Still, the estimate depends on real duty cycles, which are often recorded poorly. Use measured pressure, flow, temperature, and service hours whenever possible.
How can we help you?
Call to 0034 943884600 Contact usWe use cookies to ensure that we give you the best experience on our website. If you continue without changing your settings, we'll assume that you agree to receive cookies on the HINE website. For more information read our cookie policy page, click the link for more information.plugin cookies
ACEPTAR